Choosing a cosmetic bottle manufacturer in China starts with one decision most buyers make last: the resin. PET, PETG, PP, HDPE, acrylic and glass each behave differently with your formula, and the wrong pick shows up as a cracked shoulder or a leaking neck six weeks after delivery — long after the balance has been paid.
Bottles are harder to source than jars or tubes. They have a neck finish that must match a pump you may buy from a different plant, a wall that must survive a drop test, and a shoulder that cracks if the mould gate is placed badly.
This guide covers resin selection, neck finish standards, wall thickness, the defects specific to bottles, and the tests to run before you release payment.
Which resin fits your formula?
Start here. Every other decision follows from this one.
| Material | Best for | Clarity | Watch out for |
|---|---|---|---|
| PET | Toners, mists, water-based products | High | Poor resistance to essential oils and high-alcohol formulas |
| PETG | Serums, oils, premium clear bottles | Very high | Can craze with some essential oils — always test |
| PP | Cleansers, lotions, alcohol-based products | Translucent at best | Thin walls distort with hot fill or high alcohol |
| HDPE | Shampoo, body wash, larger volumes | Opaque | Not suitable when the customer wants to see the product |
| Acrylic (PMMA) | Outer shells for premium airless bottles | Very high, thick-wall look | Brittle, cracks on impact, never use as the product-contact layer |
| Glass | Serums, facial oils, fragrance | Highest | Weight, breakage in transit, higher freight cost |
Two rules that save whole shipments:
Never let acrylic touch the formula. Acrylic is an outer shell material. It looks like thick glass, which is why buyers love it, but it cracks under stress and reacts with many actives. The inner bottle should be PP or PETG.
Test essential oils against PETG before committing. PETG is the default choice for clear serum bottles, and it usually works. But citrus and mint oils can craze it — fine hairline cracks that appear after weeks, not days. A two-week compatibility test costs almost nothing and prevents a total loss.
The full material comparison across all pack formats is covered in our Vietnamese guide on cosmetic packaging types and how to choose.
What is a neck finish, and why does it decide your pump?
The neck finish is the thread specification at the top of the bottle. It is written as two numbers, for example 24/410.
The first number is the outer diameter of the neck in millimetres. The second is a thread style code that defines the thread profile and the height of the closure.
| Common finish | Typically used for | Note |
|---|---|---|
| 18/410 | Small serum and treatment bottles | Pairs with small lotion pumps and droppers |
| 20/410 | Toners, small mists | Very widely stocked, easy to source closures |
| 24/410 | Lotion bottles, cleansers | The most common size in skincare |
| 28/410 | Shampoo, body wash, larger formats | Higher output pumps |
| 24/415 | Same diameter as 24/410, taller thread | Not interchangeable — a 410 pump will not seat correctly |
The last row is where money gets lost. 24/410 and 24/415 share a diameter, so the pump appears to fit. It threads on, it looks fine, and it leaks in transit because the seal never fully compresses.
Two practical rules:
- Buy the bottle and the closure as a matched set whenever possible. If they come from different plants, send a physical bottle sample to the closure supplier rather than sending a drawing.
- Always assemble and test before mass production. Fill, cap, invert and leave for 48 hours. Then repeat after a transport vibration test if you can.
Ask your supplier which finishes they already tool. Using a finish they stock means faster samples and easier closure sourcing later.
How much wall thickness do you actually need?
Wall thickness is the quietest cost lever in bottle sourcing, and the easiest place for a supplier to shave margin without telling you.
Thinner walls use less resin and cost less. They also dent under grip pressure, deform under stacking load in the carton, and crack at the shoulder when dropped.
| Symptom | Likely cause | What to ask |
|---|---|---|
| Bottle dents when held normally | Wall too thin overall | Ask for the bottle weight in grams, not the thickness |
| Cracks at the shoulder | Uneven material distribution during blowing | Ask to see a section cut through the shoulder |
| Base pushes inward | Insufficient base thickness or bad base design | Ask for a top-load test result |
| Bottles deform in stacked cartons | Top-load strength too low | Specify a minimum top-load value in the agreement |
The most useful specification to control is bottle weight in grams, not wall thickness in millimetres. Weight is easy to verify with a scale on the receiving bench. Thickness varies point to point and needs a section cut to measure.
Write the target weight and an acceptable tolerance into the specification annex, and check it during inspection. A supplier who quietly drops two grams per bottle across a 50,000 piece order has made a meaningful saving at the cost of your drop test.
Which defects are specific to bottles?
Jars and tubes have their own failure modes. These seven belong to bottles.
- Shoulder cracking. Material stretched too thin where the body narrows into the neck. Shows up in drop tests and during shipping.
- Neck ovality. The neck is not perfectly round, so the closure seals on one side and leaks on the other.
- Gate mark on the base. A raised or sharp mark where the material entered. Makes the bottle rock instead of standing flat.
- Weld line down the body. A visible seam where two material flows met. Cosmetically obvious on clear bottles.
- Uneven wall distribution. One side noticeably thinner. Often invisible until the bottle is squeezed or dropped.
- Base push-up failure. The base bulges outward so the bottle will not stand level once filled.
- Haze in clear resin. Cloudiness from moisture in the resin or from regrind content that was not disclosed.
Defect seven deserves a direct question during supplier selection: what percentage of regrind is used, and is it in-house scrap only? Recycled content is legitimate and often desirable, but it must be declared, controlled and consistent — not a silent way to lower cost.
Defects two and five are the ones that survive a visual inspection and fail in the field. Both need physical checks, not a look.
Which tests should you run before releasing the balance?
| Test | How to run it | Catches |
|---|---|---|
| Weight check | Weigh a random sample against the agreed target and tolerance | Silent wall thinning |
| Neck gauge check | Thread a reference closure onto samples from across the lot | Neck ovality, wrong finish |
| Leak test | Fill, cap, invert, leave 48 hours; repeat after vibration if possible | Sealing failures, neck defects |
| Drop test | Drop filled and capped bottles from shelf height onto a hard floor | Shoulder cracking, thin walls |
| Top-load test | Apply vertical load to a standing bottle | Stack collapse in cartons |
| Compatibility test | Fill with your actual formula, hold at room and elevated temperature | Crazing, deformation, print lifting |
| Print adhesion | Rub the printed area firmly, then tape-pull it | Decoration that will not survive handling |
Run the compatibility test early — during sampling, not during inspection. It takes weeks, and it is the only test that can invalidate the entire material choice.
Run the other six at inspection, before the balance is paid. Once the container has sailed, your leverage is gone.
Should you tool a custom bottle mould?
Usually not, at least not for a first order.
| Option | When it makes sense | Trade-off |
|---|---|---|
| Stock mould, stock colour | First production run, testing the market | Your bottle looks like other brands using the same mould |
| Stock mould, custom decoration | You need a distinct look on a modest budget | Shape is shared, but the finished look is yours |
| Stock mould, custom colour | Colour is central to the brand identity | Higher minimum because masterbatch is mixed in batches |
| Custom mould | Volume is proven and the shape is a real differentiator | Tooling cost, longer lead time, and mould ownership must be agreed |
For most brands, the second row gives the best return. A stock shape with a distinctive frosted finish, a custom colour cap and a well-executed silk-screen reads as a designed product, at a fraction of the cost and time.
If you do tool a custom mould, settle three things in writing before paying: who owns the mould after payment, where it is stored, and whether it can be moved to another factory. A mould you paid for but cannot move is not yours in any practical sense.
Minimum order quantities by level of customisation are covered in our Vietnamese guide on minimum order quantities for cosmetic packaging.
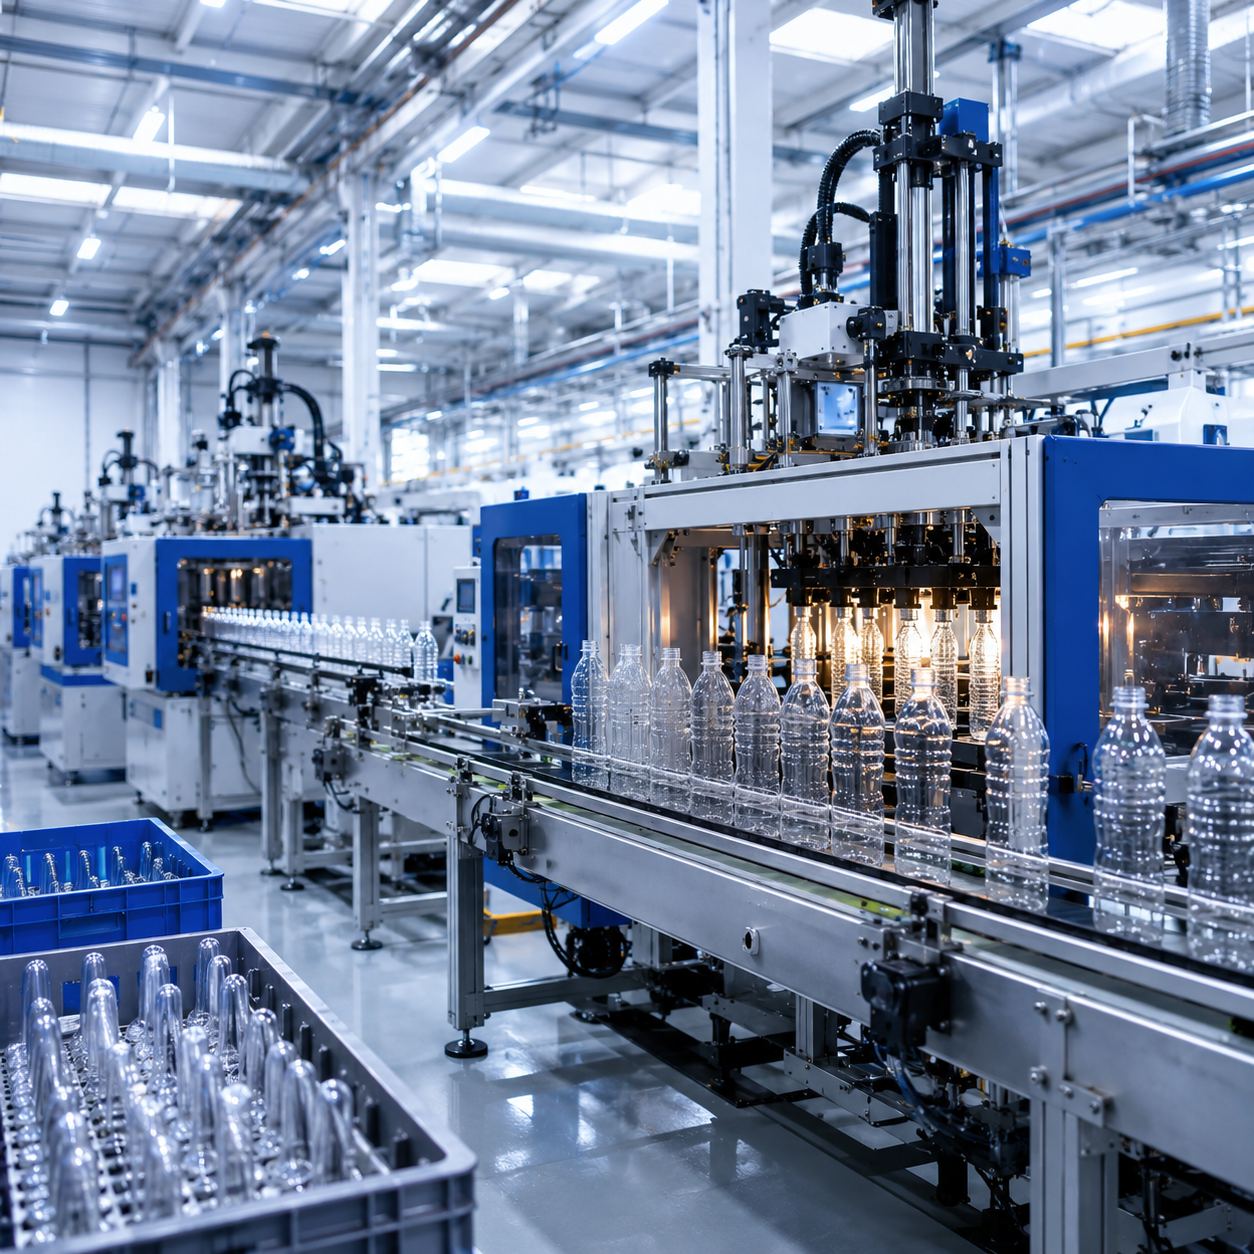
How do you tell a real bottle factory from a reseller?
Bottle plants are capital-heavy. A real one has blow moulding machines on site and can answer machine-level questions immediately.
Four questions that separate them:
- Which blowing process do you use for this bottle — extrusion blow or injection stretch blow? PET and PETG bottles are normally injection stretch blow moulded; HDPE and PP are often extrusion blow moulded. A factory answers without pausing.
- How many cavities is the mould for this item? This determines output per hour and is a number the workshop knows.
- Which neck finishes do you already tool? A factory has a list. A reseller says “any finish you want”.
- Can you send a dated photo of my part on the line? The simplest test of all.
None of this makes a trading company a bad partner. Trading companies are useful when you need a mixed order across several product types in modest quantities. The point is to know which one you are dealing with, so your expectations about quality control and lead time are realistic.
The full comparison between factory direct, trading company and sourcing partner is in our guide on cosmetic packaging manufacturing in China.
Checklist before your first bottle order
- Has the resin been chosen based on your actual formula, not on appearance?
- Has the compatibility test been run at room and elevated temperature?
- Is the neck finish written in full, including the thread code, not just the diameter?
- Have bottle and closure been assembled and leak tested together?
- Is the target bottle weight in grams written into the specification with a tolerance?
- Has a drop test been run on filled and capped samples?
- Is the regrind percentage declared and agreed?
- Is there a signed and sealed reference sample held by both parties?
- If a custom mould is involved, are ownership, storage and transfer written down?
- Is the balance payable after inspection rather than before shipment?
The third item causes more shipment failures than any other on this list. Writing “24mm neck” instead of “24/410” leaves the thread code open, and the factory will pick whichever one they already tool.
Browse available bottle moulds in our catalogue, including all-plastic PETG dropper bottles in 30ml, PP lotion pump bottles with a 24/410 finish and airless bottles in 15ml, 30ml and 50ml.
About VEENI
VEENI — SẢN XUẤT GIA CÔNG CHAI LỌ MỸ PHẨM TẠI TRUNG QUỐC
Cosmetic packaging manufacturing and sourcing in China.
What we do: design consulting, supplier sourcing, sample development, production management at the factory, and import handling. Our import experience is primarily into Vietnam — if you need delivery to another market, tell us the destination and we will confirm what we can arrange before you commit to anything.
- Hotline: 0933 439 668
- Email: Veenivietnam@gmail.com
- Address: LK 15-VT29, Khu nhà ở Xa La, P. Phúc La, Q. Hà Đông, Hà Nội, Vietnam
Frequently asked questions
Which plastic is best for cosmetic bottles?
It depends on the formula. PET suits toners and water-based products. PETG gives the best clarity for serums and oils but should be tested against essential oils first. PP handles alcohol-based products and cleansers. HDPE suits shampoo and larger opaque formats. Acrylic is an outer shell material only and should never contact the product.
What does 24/410 mean on a cosmetic bottle?
It is the neck finish. 24 is the outer diameter of the neck in millimetres, and 410 is a thread style code defining the thread profile and closure height. Note that 24/410 and 24/415 share a diameter but are not interchangeable — a 410 pump will thread onto a 415 neck and still leak.
How do I stop bottles cracking at the shoulder?
Shoulder cracking comes from material being stretched too thin where the body narrows into the neck. Specify a target bottle weight in grams with a tolerance, ask to see a section cut through the shoulder, and run a drop test on filled and capped samples before releasing the balance.
Should I order a custom bottle mould for my first run?
Usually not. A stock mould with custom decoration — a frosted finish, a custom colour cap and good silk-screen printing — reads as a designed product at a fraction of the tooling cost and lead time. Consider a custom mould once volume is proven and the shape is genuinely a differentiator.
What tests should be done before paying the balance?
Weight check against the agreed target, neck gauge check with a reference closure, leak test after filling and inverting for 48 hours, drop test from shelf height, top-load test, and print adhesion. The compatibility test with your actual formula should be run earlier, during sampling, because it takes weeks.
Related articles
- Cosmetic packaging manufacturer in China: factory direct sourcing guide
- Cosmetic packaging types and how to choose (Vietnamese)
- Minimum order quantities for cosmetic packaging (Vietnamese)
- Serum bottles: formats and materials (Vietnamese)
- Sourcing cosmetic packaging from China (Vietnamese)